Heavy Equipment Machining Case Study
Background
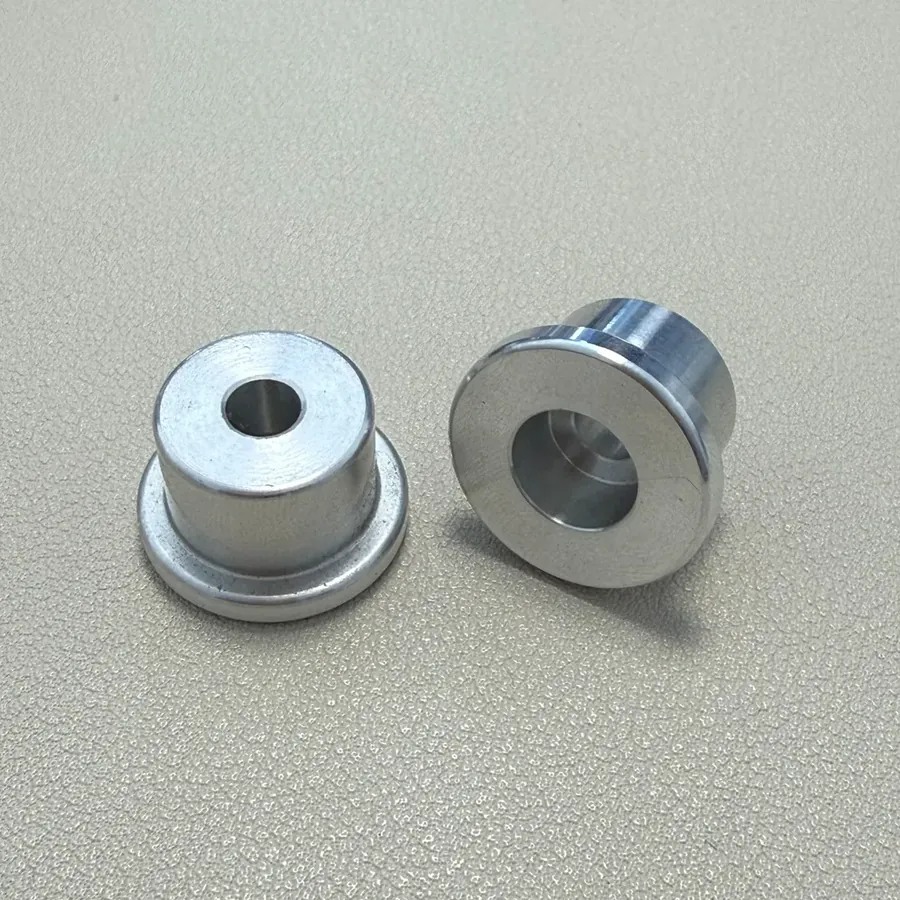
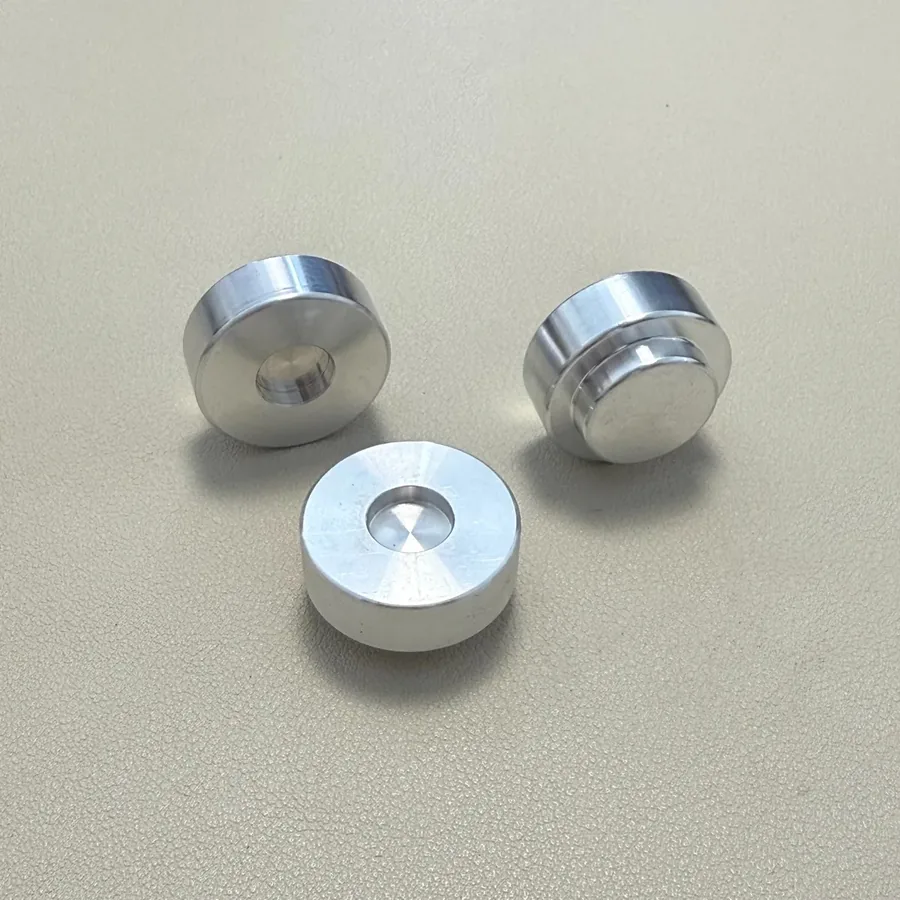
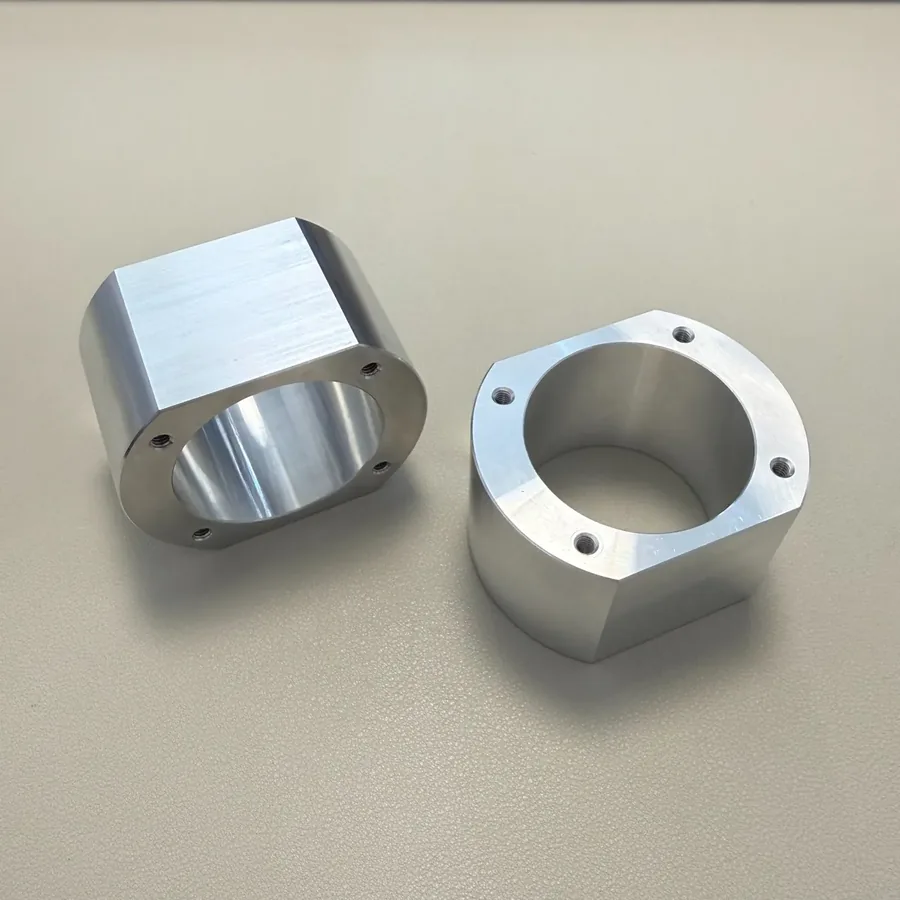
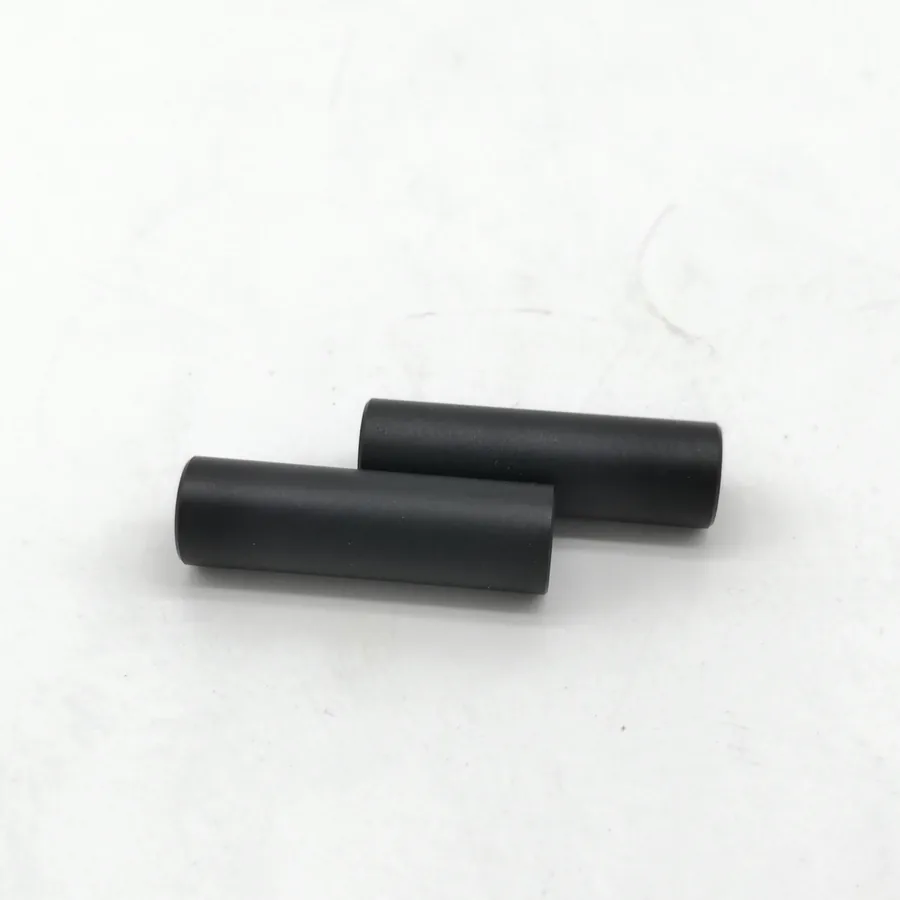
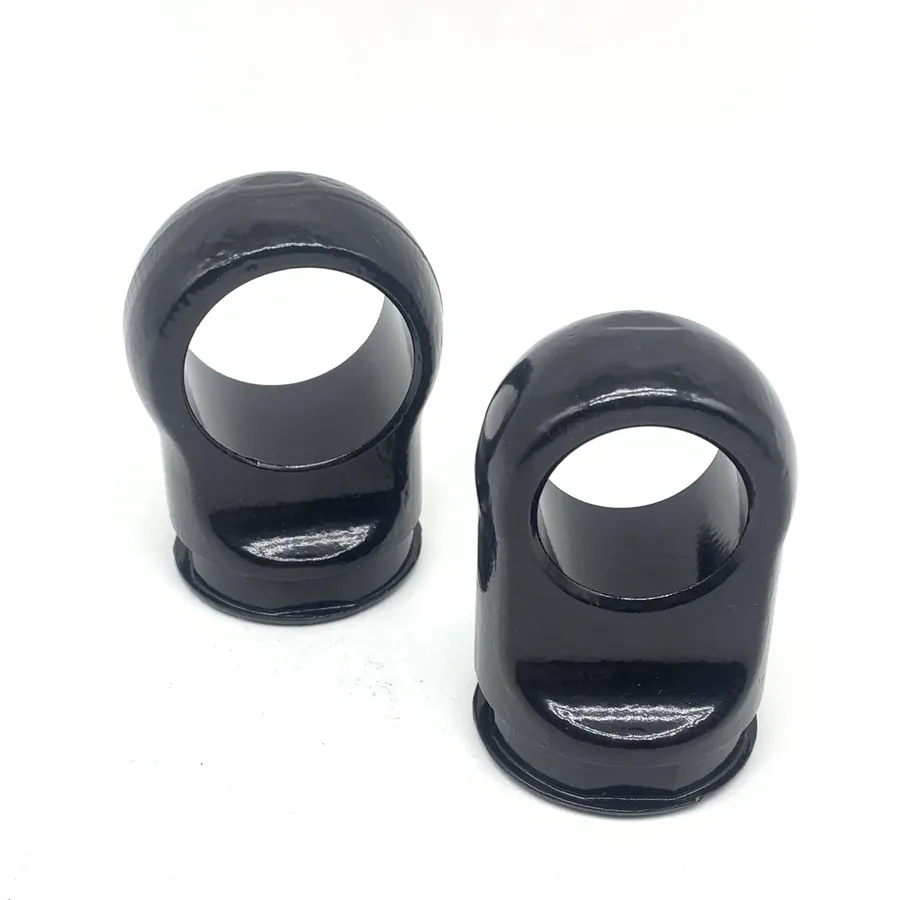
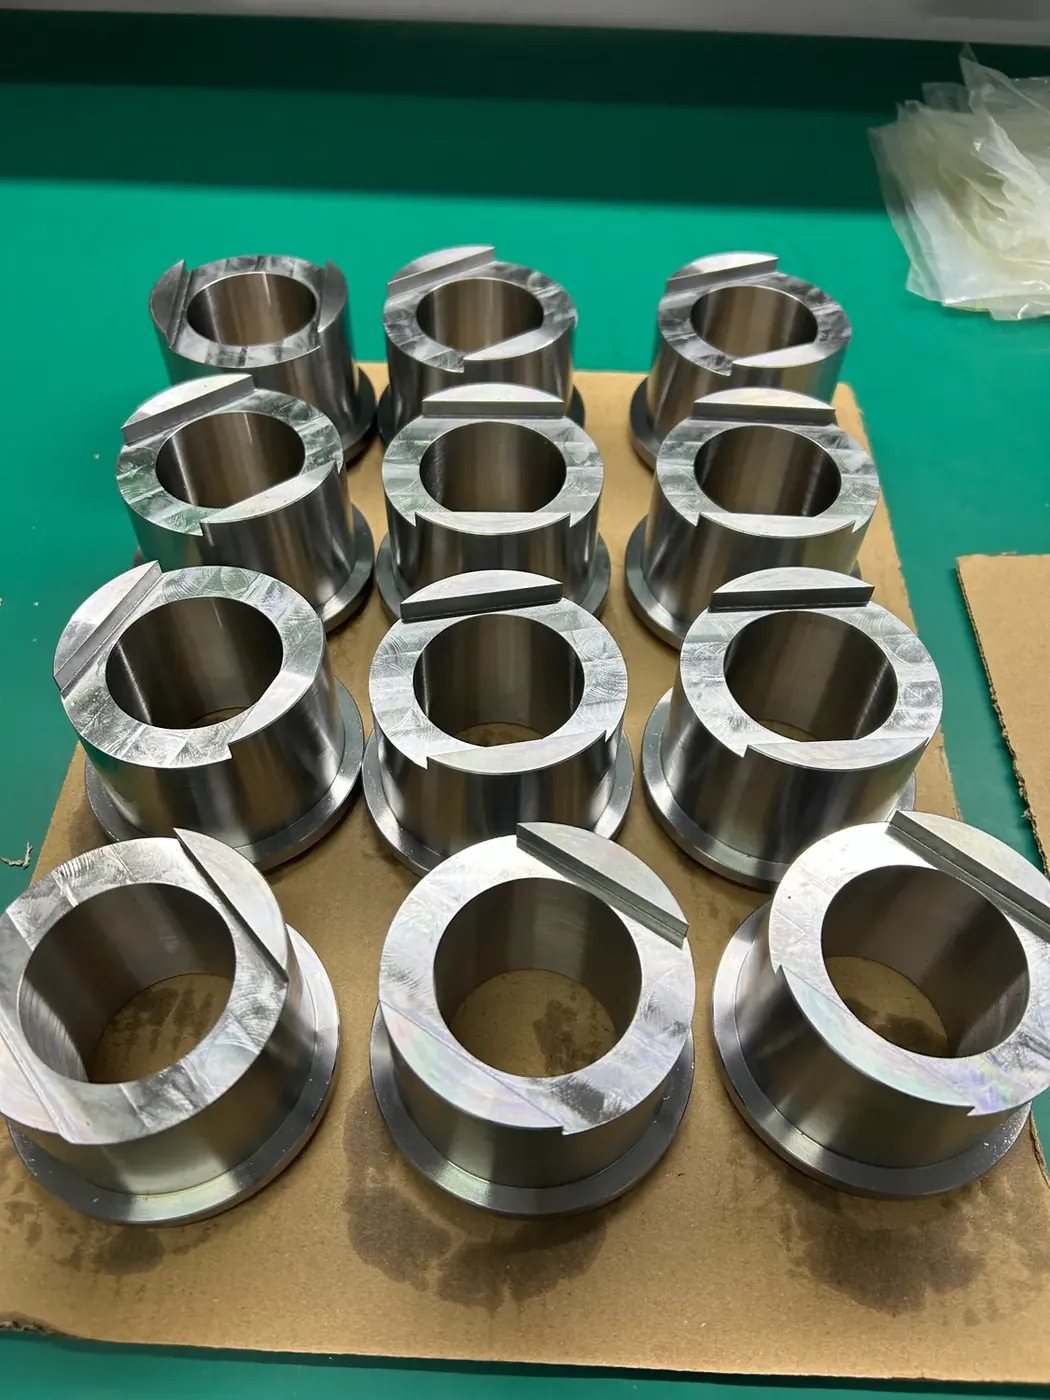
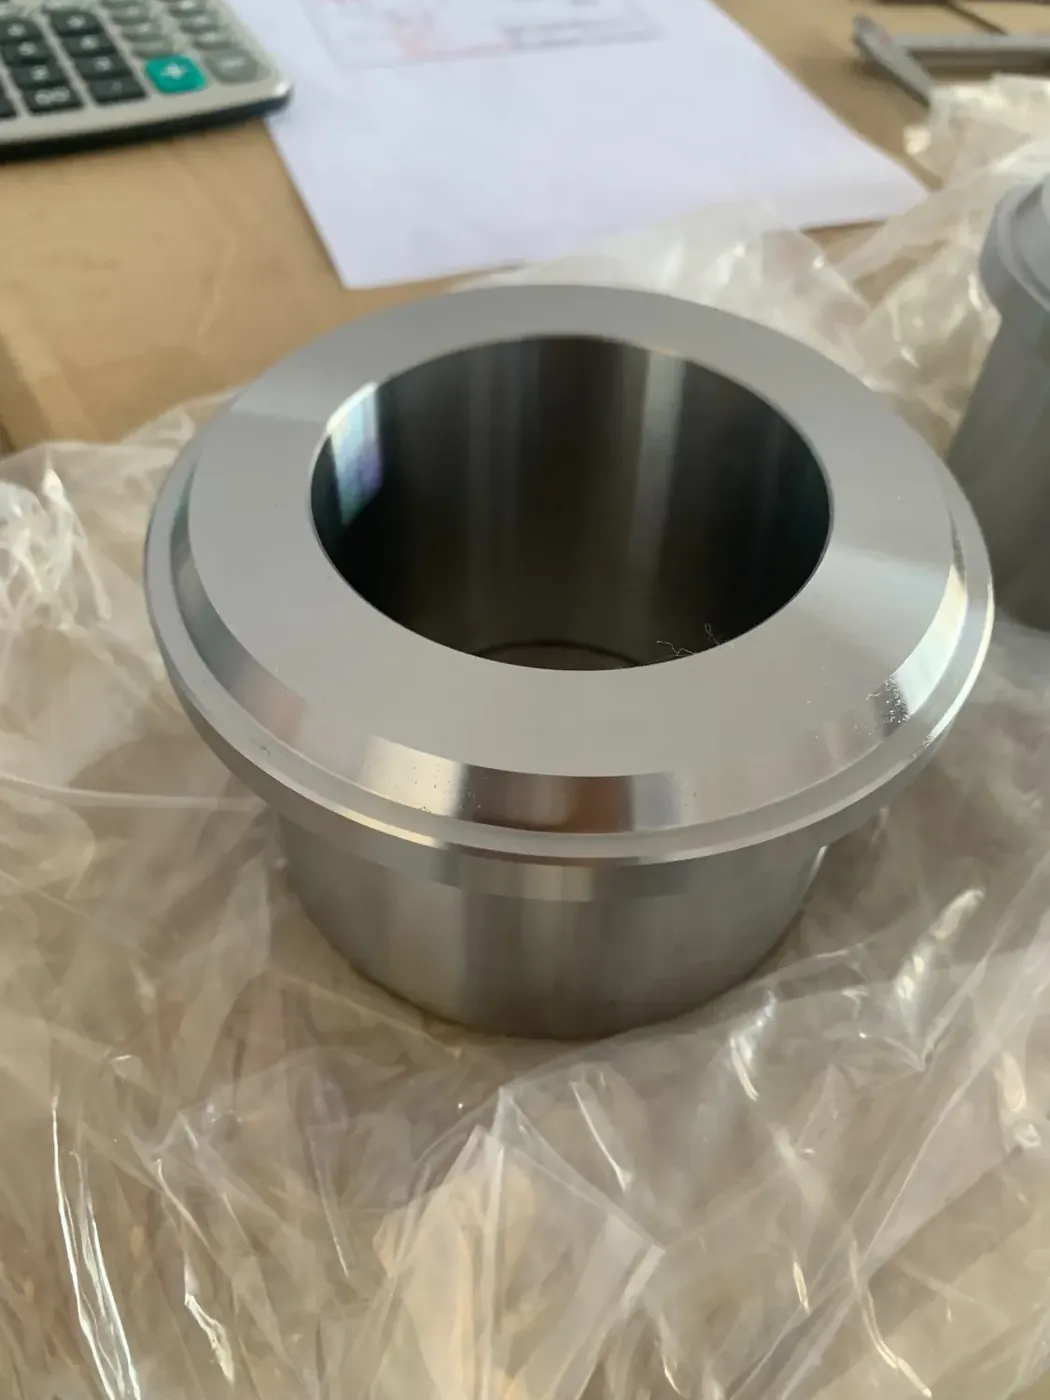
This recurring program covers paired bushing components used in excavator attachment assemblies. The two components serve different roles: a machinable outer seat provides the installation interface, while a separate wear bushing carries the hardened internal surface and lubrication features.
The parts are straightforward in appearance, but the assembly depends on two different manufacturing routes coming together consistently. Exact customer grades, hardness values, dimensions and fit data are intentionally omitted from this public case study.
The Challenge
The main challenge is not complex geometry; it is controlling a two-component system across different process routes. The outer component can be machined in the soft condition, while the inner wear bushing requires alloy steel, internal lubrication grooves, heat treatment and finish grinding on critical surfaces.
Those routes then converge at press-fit assembly. Excessive interference can make assembly difficult or damage the mating components, while insufficient interference can reduce retention. The fit therefore depends on dimensional control across machining, heat treatment and grinding rather than on one operation alone.
Because the program includes multiple similar-looking variants, repeat production also depends on correct routing, identification and drawing control. The practical objective is not to make one good sample, but to maintain the same assembly behavior over recurring orders.
Our Approach
We manage the two component types as separate manufacturing routes and bring them together only after the wear bushing has completed heat treatment and final dimensional finishing. This keeps the soft outer component economical to machine while allowing the inner component to provide the required wear resistance and controlled fit.
Two Routes, One Press-Fit Assembly
Soft-state CNC machining
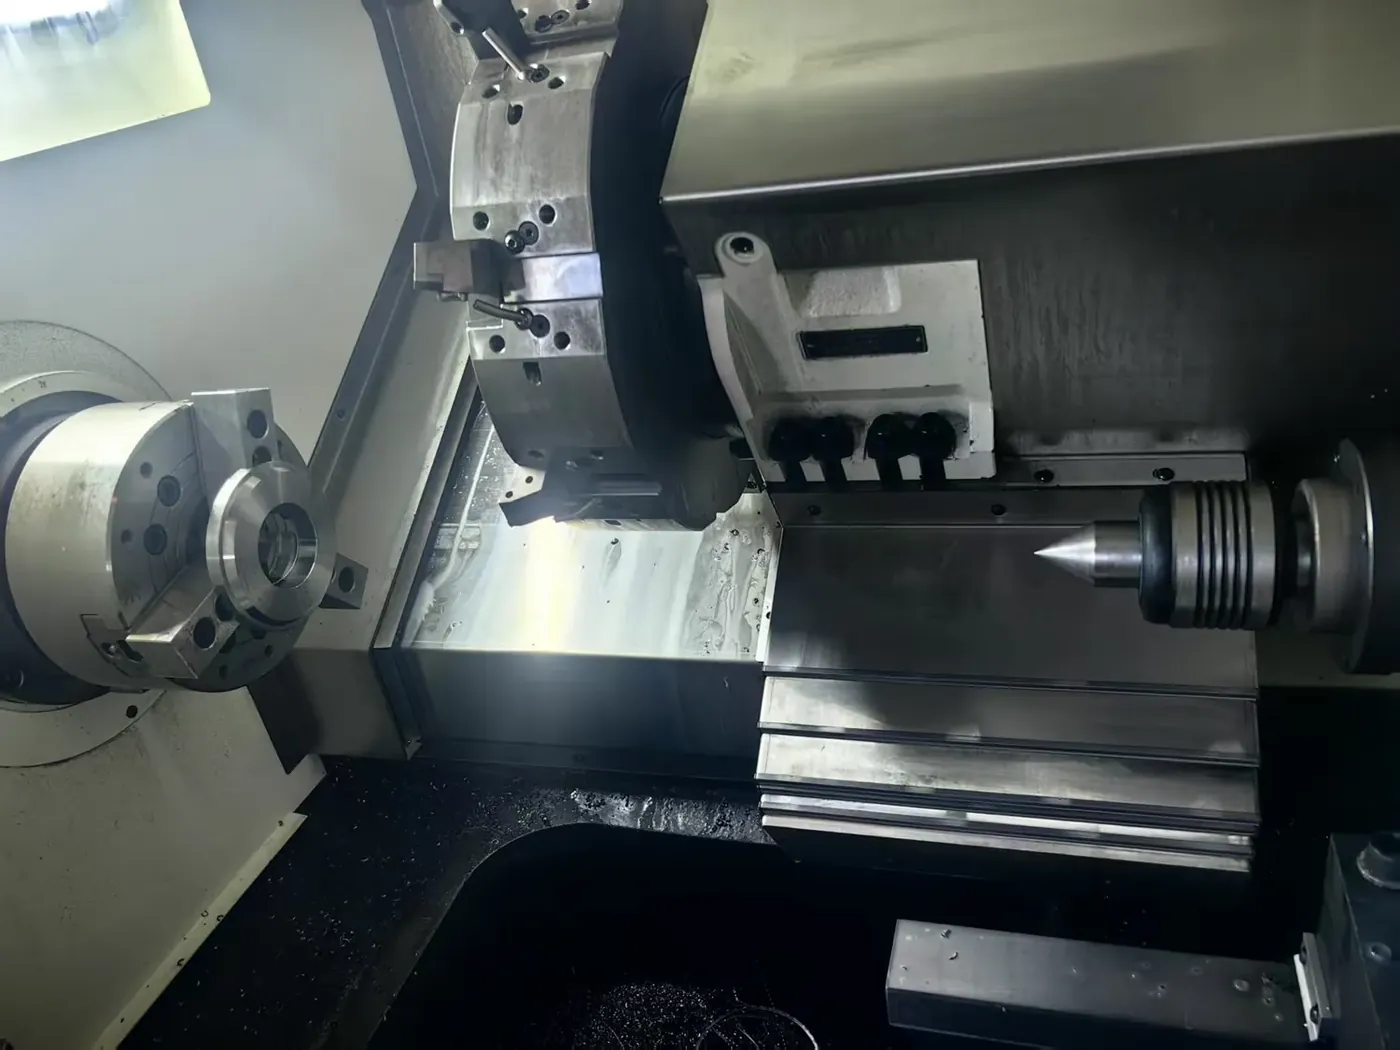
The outer component is produced as a machinable carbon-steel seat. Turning and secondary features establish the interface without a hardening operation.
Heat treatment + finish grinding
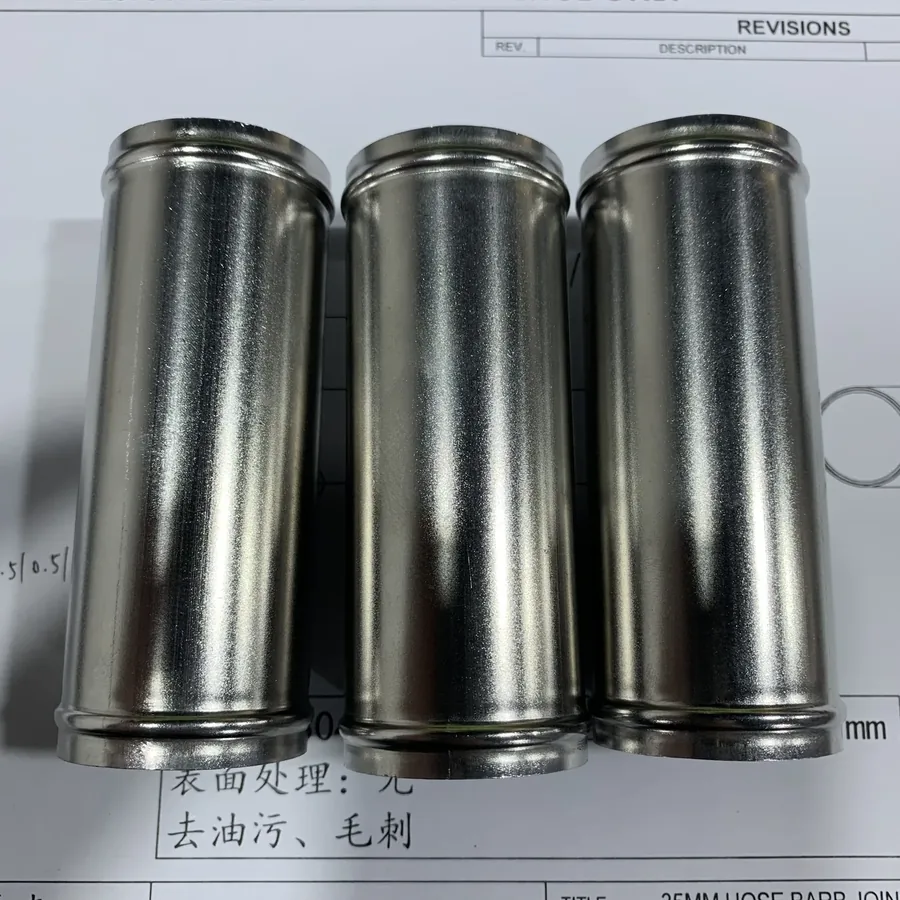
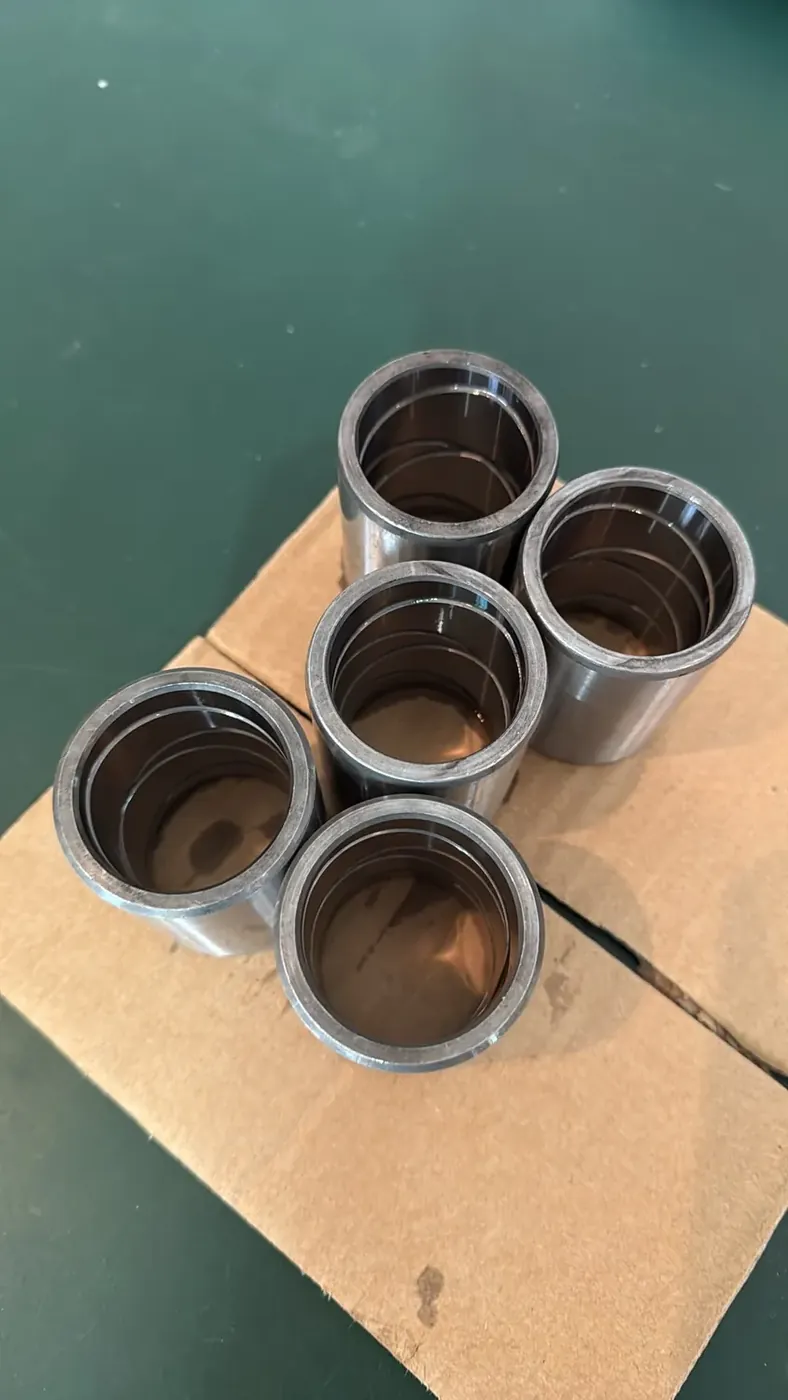
The inner bushing is machined from alloy steel with internal lubrication grooves, then heat treated and finish-ground on the critical ID / OD surfaces.
Controlled press-fit assembly
The finished wear bushing is pressed into the outer component after final dimensional verification. The fit is controlled as an assembly requirement rather than treated as two unrelated turned parts.
Repeat-Production Control
Installed in Heavy-Equipment Attachments
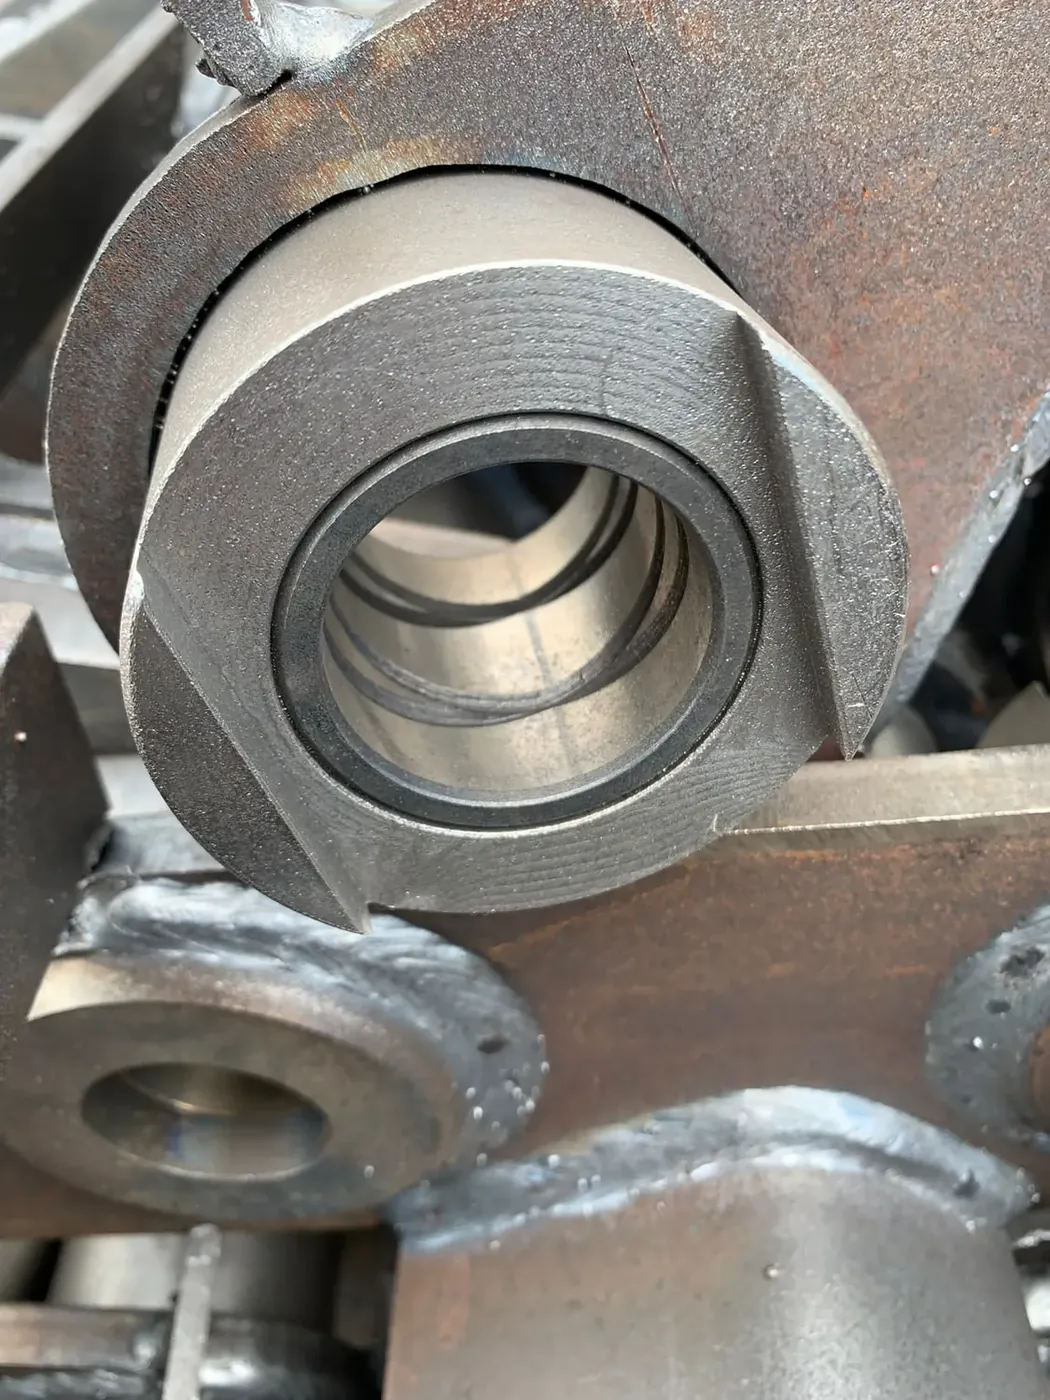
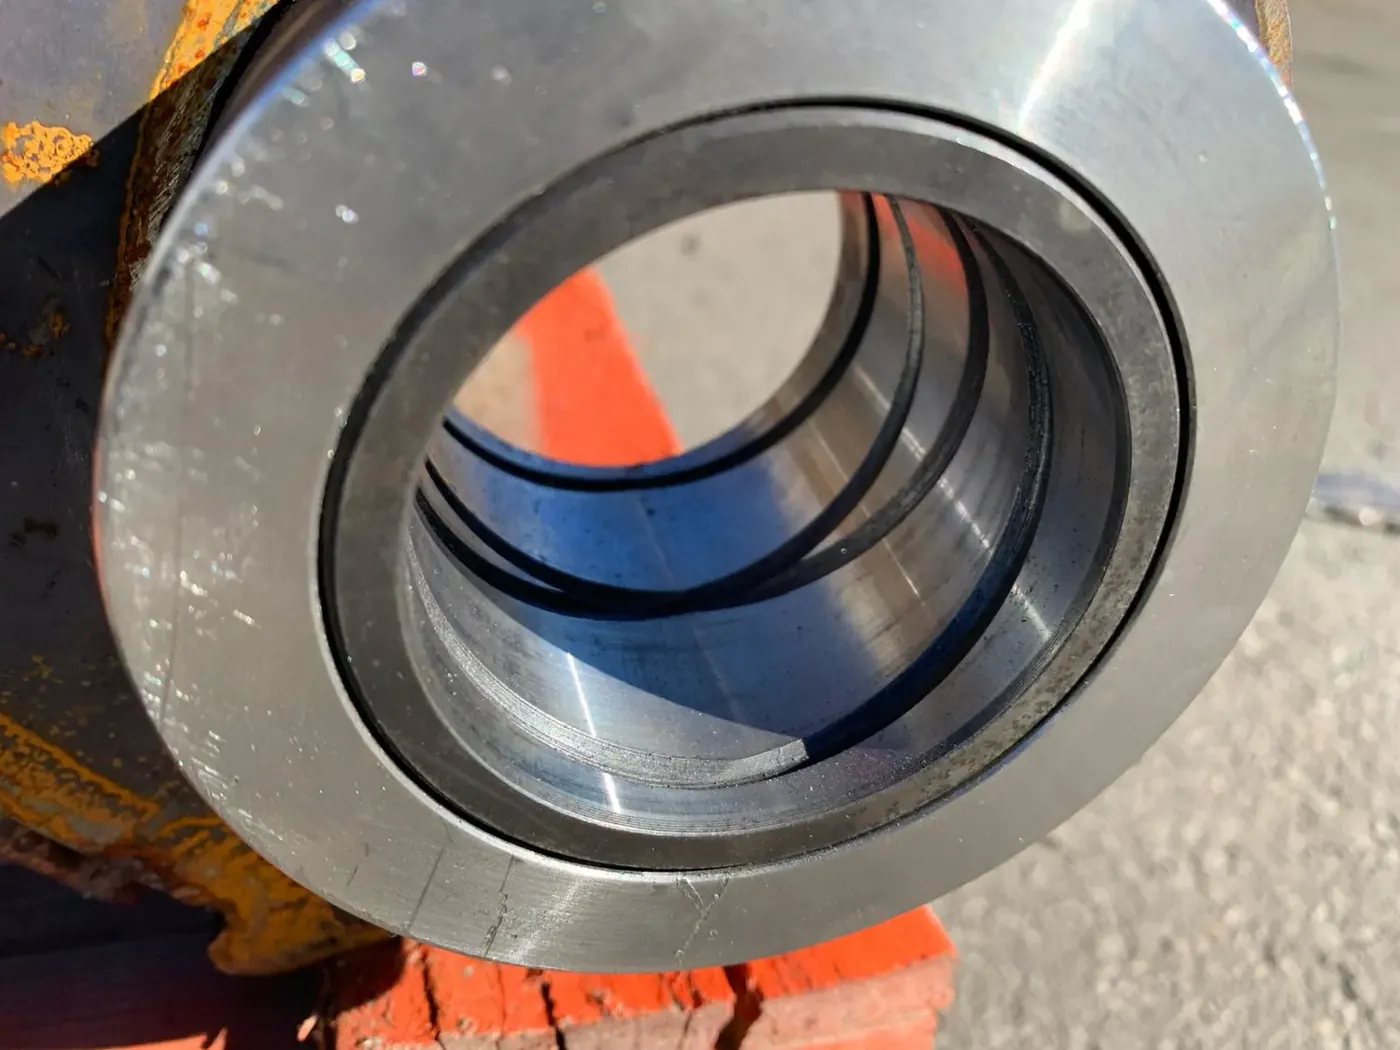
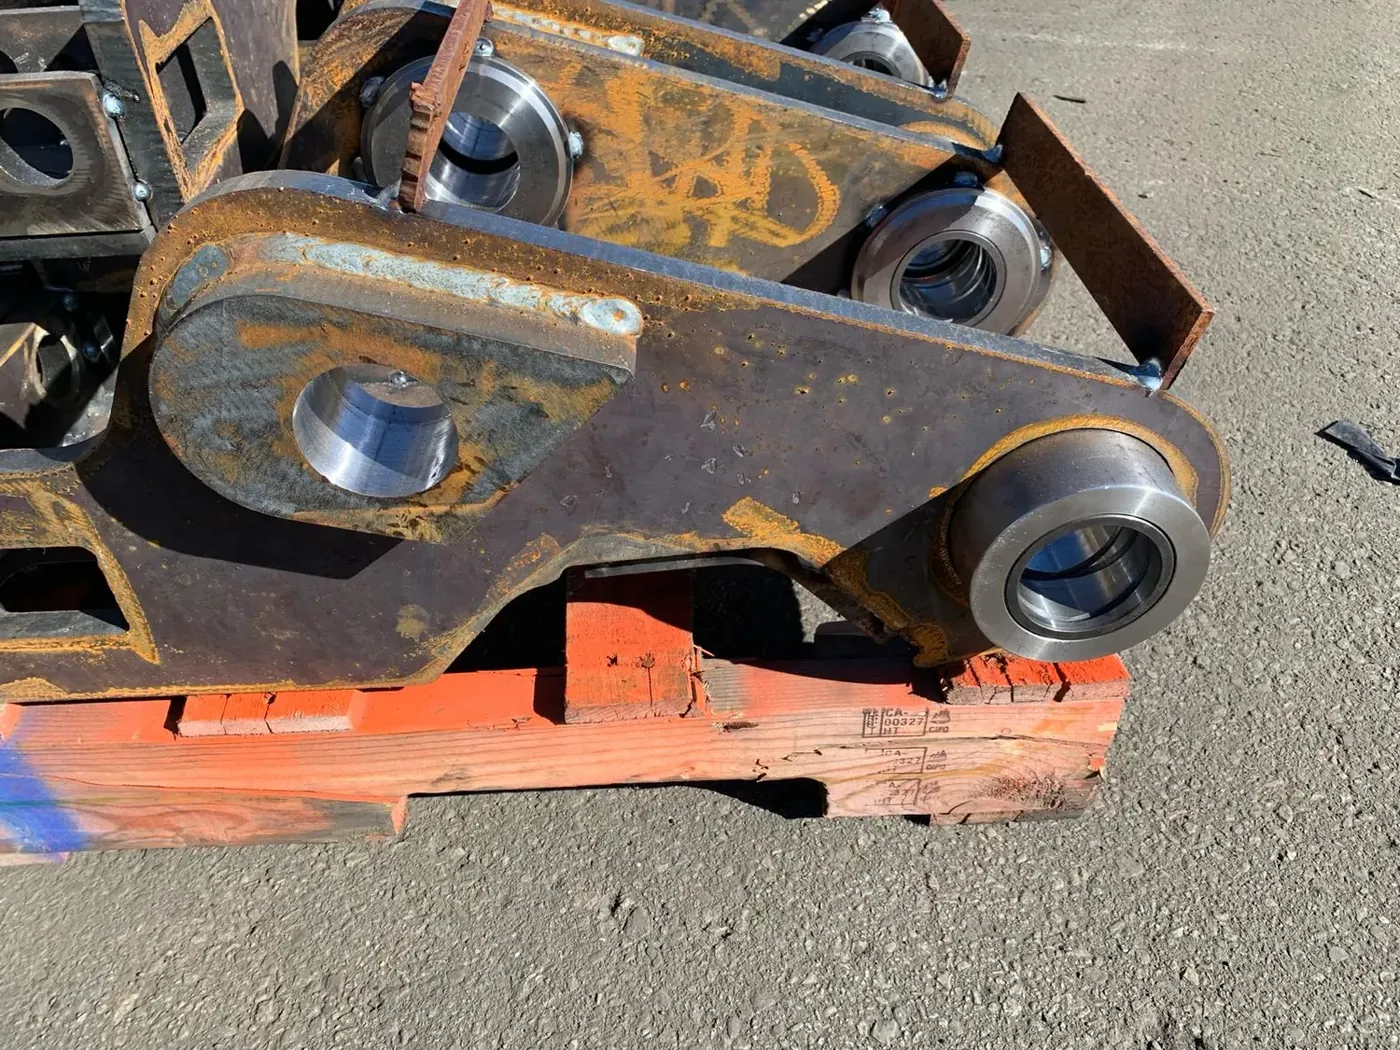
Installation photos are shown only at a general level. They confirm the end-use context without publishing customer-specific drawings, part numbers or assembly dimensions. In the finished equipment, the bushing assembly becomes one wear-controlled interface inside a much larger fabricated attachment.
Result
This has become a stable repeat-production program rather than a one-time prototype job. Its value lies in coordinating two material and process routes, controlling the final press-fit relationship and keeping multiple related variants correctly identified through recurring orders.
For similar heavy-equipment wear components, we can review the drawing, material family, heat-treatment requirement, fit strategy and inspection scope without requiring the customer to disclose more application detail than is necessary for manufacturing.